Surface Treatment Is a System, Not a Product.
Chemistry engineered to your water profile, throughput, and compliance requirements. Since 1993, MacroCoats has served India's most demanding industrial clients — from Indian Railways to Tier-1 automotive OEMs.
We Begin With
Your Constraints.
Most suppliers deliver a concentrate and leave. MacroCoats engineers the full pre-treatment system — from your first rinse tank to your final passivation stage.
The result holds specification across every shift, every operator, and every season. Not because your operators are more attentive — because the system doesn't wait for them to act.
Every molecule matched to your incoming water hardness, chloride load, and dissolved iron. Real process intelligence, not guesswork.
Salt spray validation, paint adhesion testing, crystal microscopy. Every batch certified before dispatch.
REACH-registered, RoHS-compliant, EU ELV-certified, IS 6005:2011, ISO 9001:2015, BIS-approved. Chrome-free options available.
Four stages. One continuous system.
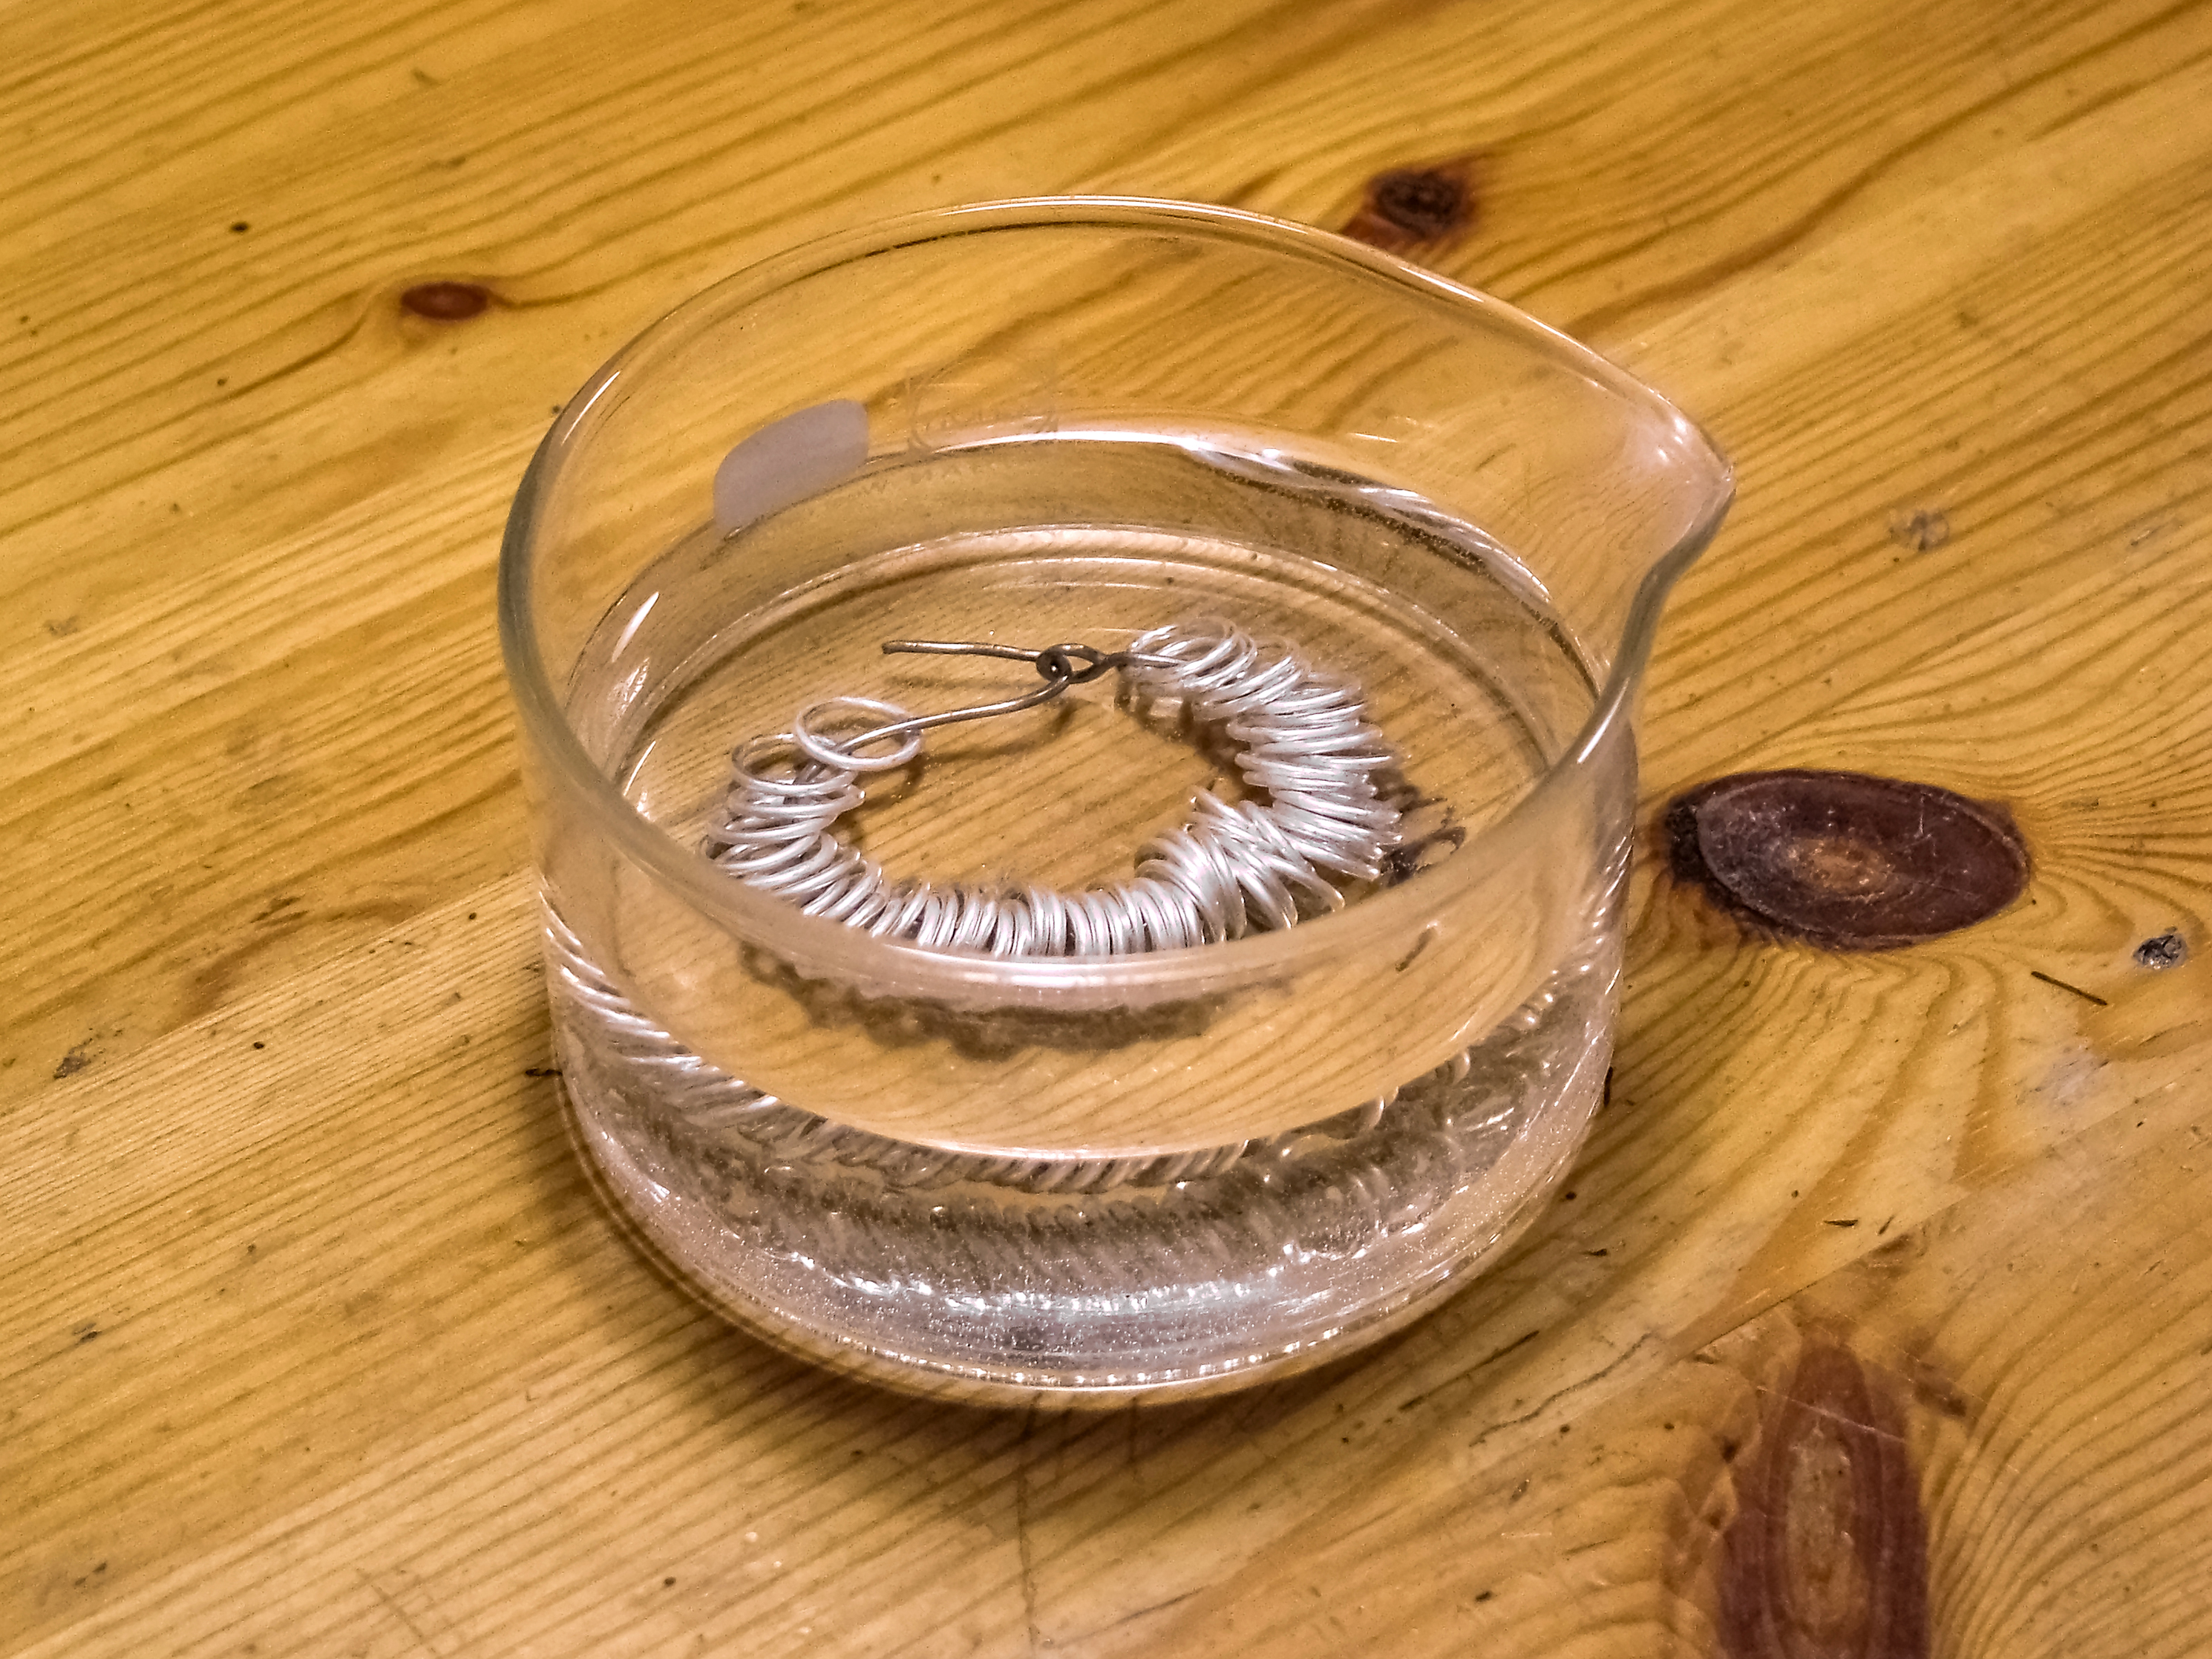
Surface Preparation
No conversion coating chemistry — however precisely formulated — will bond to a contaminated surface. Stage one removes oil, mill scale, and metallic oxides through a sequenced alkaline degrease, acid pickle, and activation step. Each chemistry in this sequence is engineered for the specific soil type and base metal on your line.
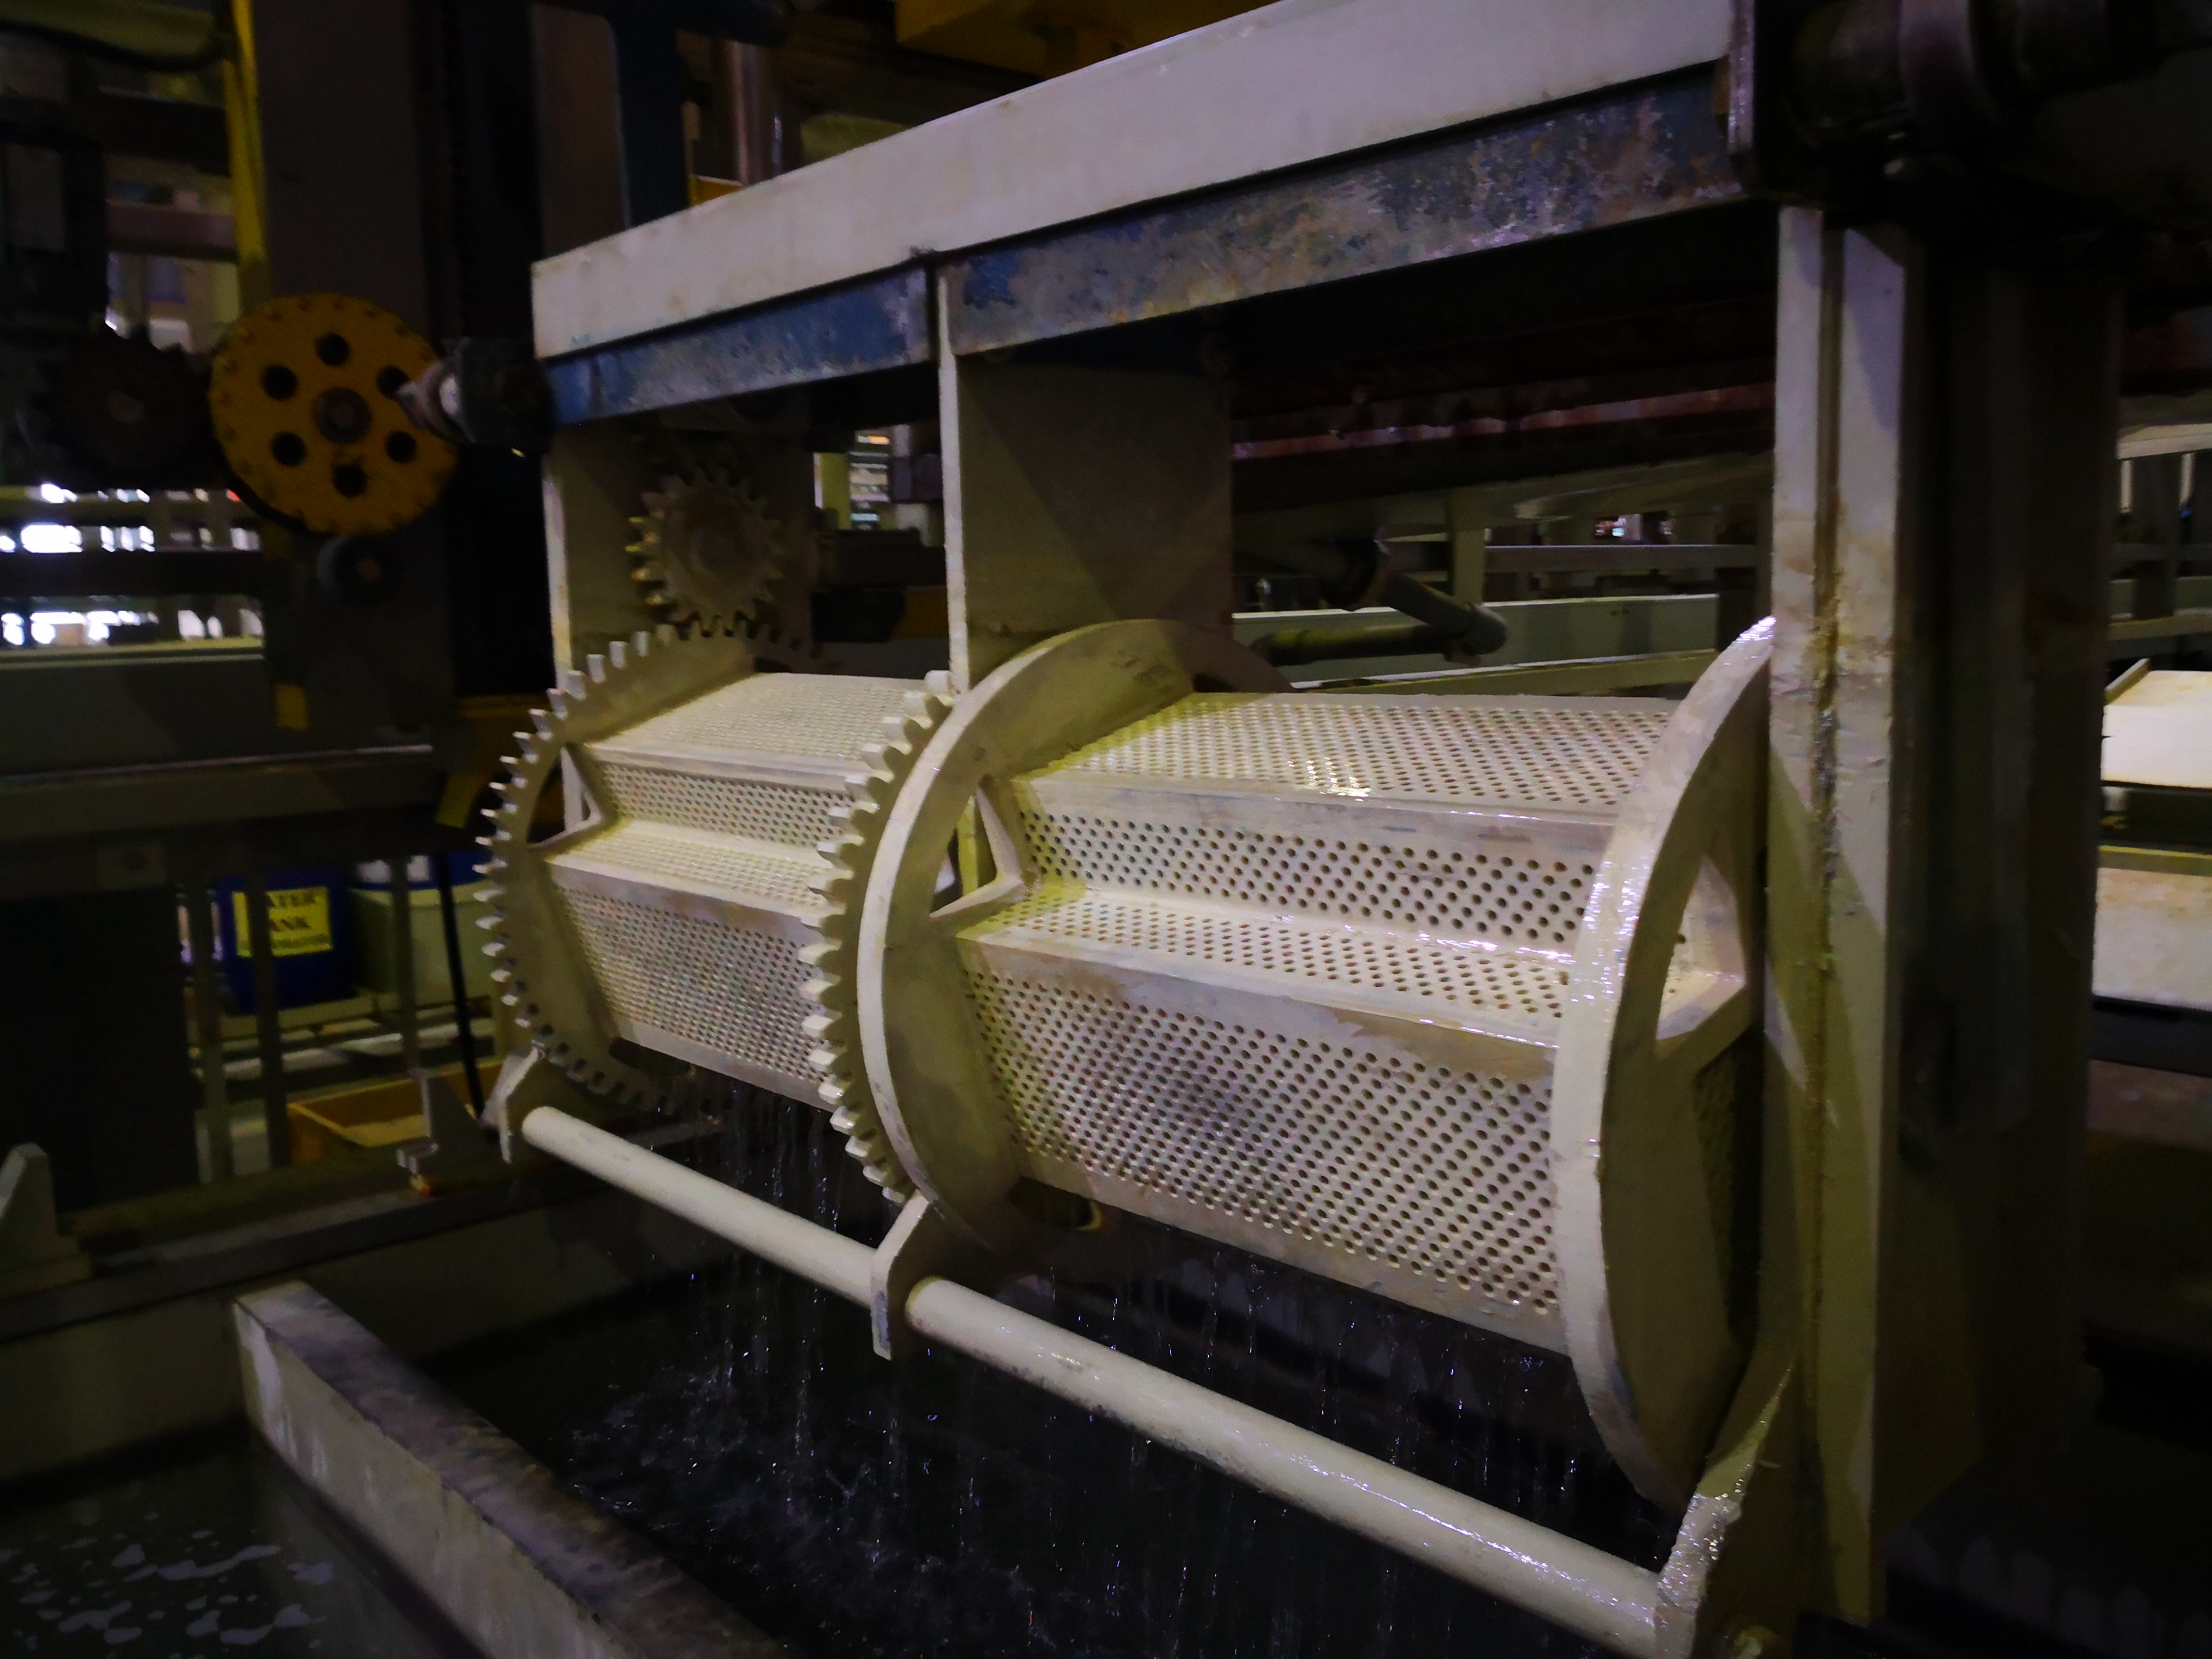
Conversion Coating
The phosphating reaction converts the bare metal surface into an insoluble crystalline layer bonded directly to the substrate. Crystal composition — zinc, iron, or manganese — is chosen for the downstream requirement: zinc for paint adhesion, manganese for wear surfaces, iron for light-duty pre-paint. Bath chemistry is held within tight limits throughout the production shift.
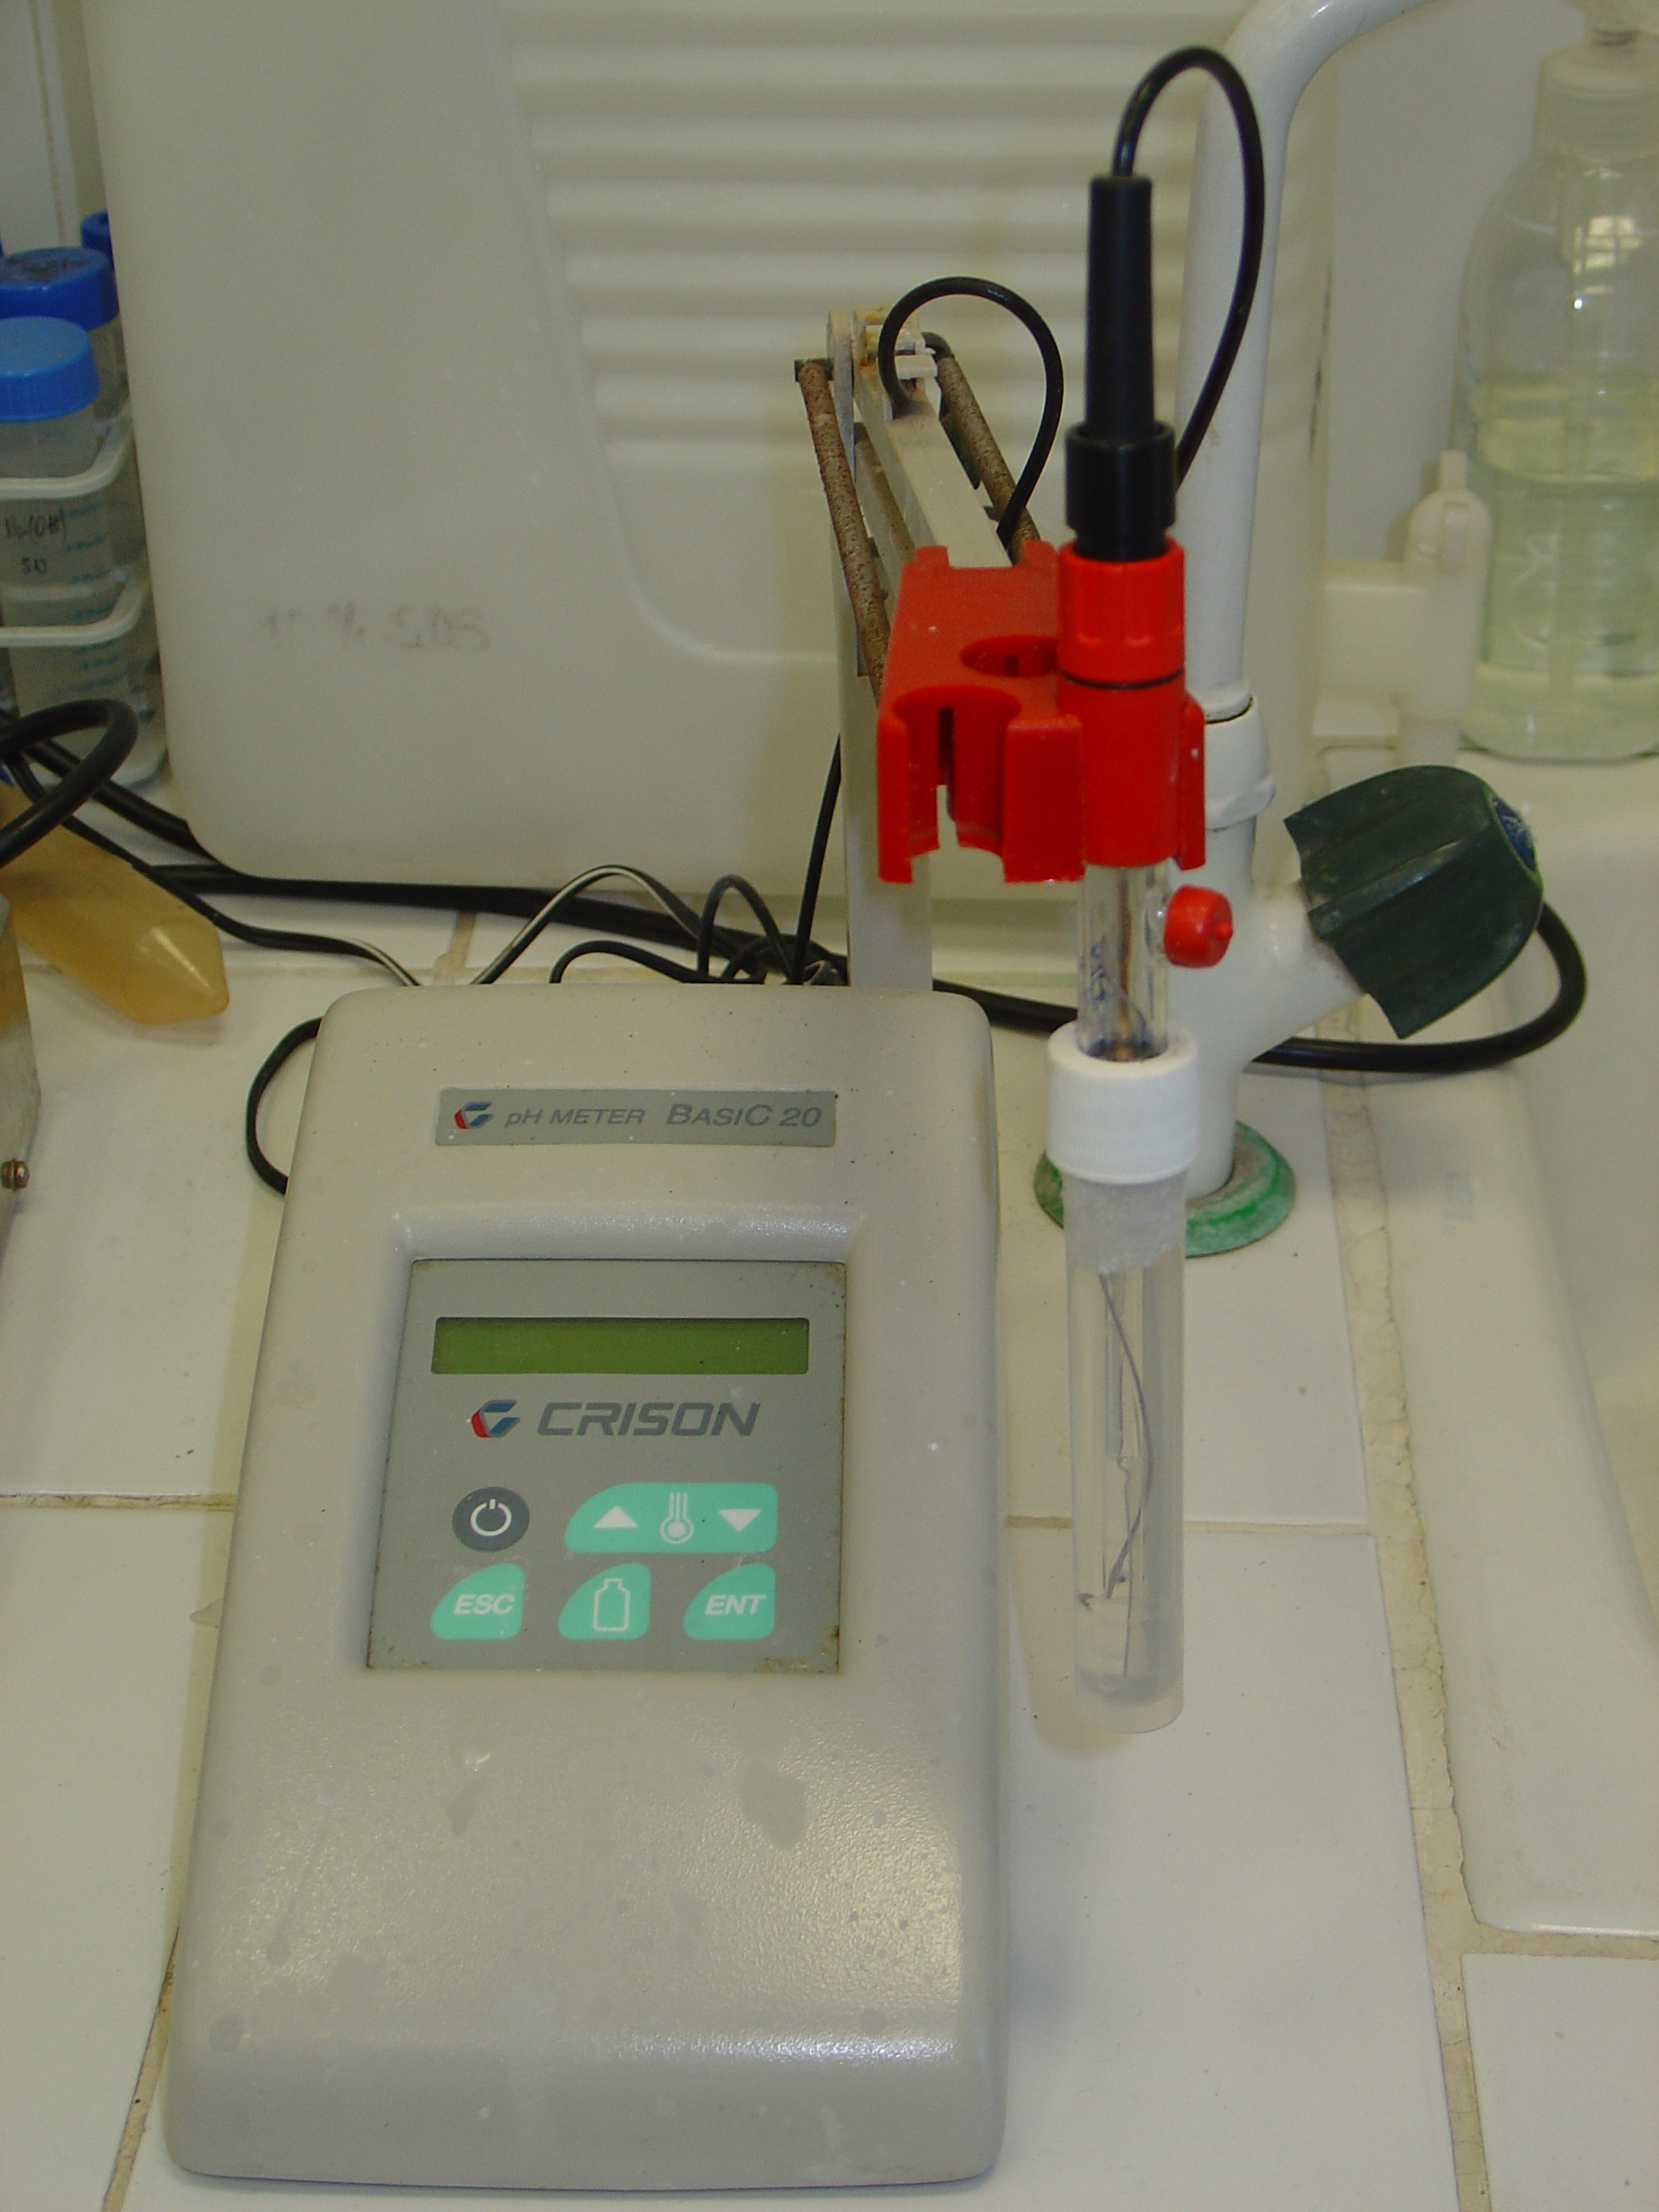
In-Process Verification
Coating weight, crystal morphology, and bath parameters are verified against specification at defined intervals — not inspected after parts have failed salt-spray. Point weight titration and pH measurement confirm bath health before each production run. IoT sensors extend this verification continuously, triggering auto-dose corrections before the bath drifts out of range.
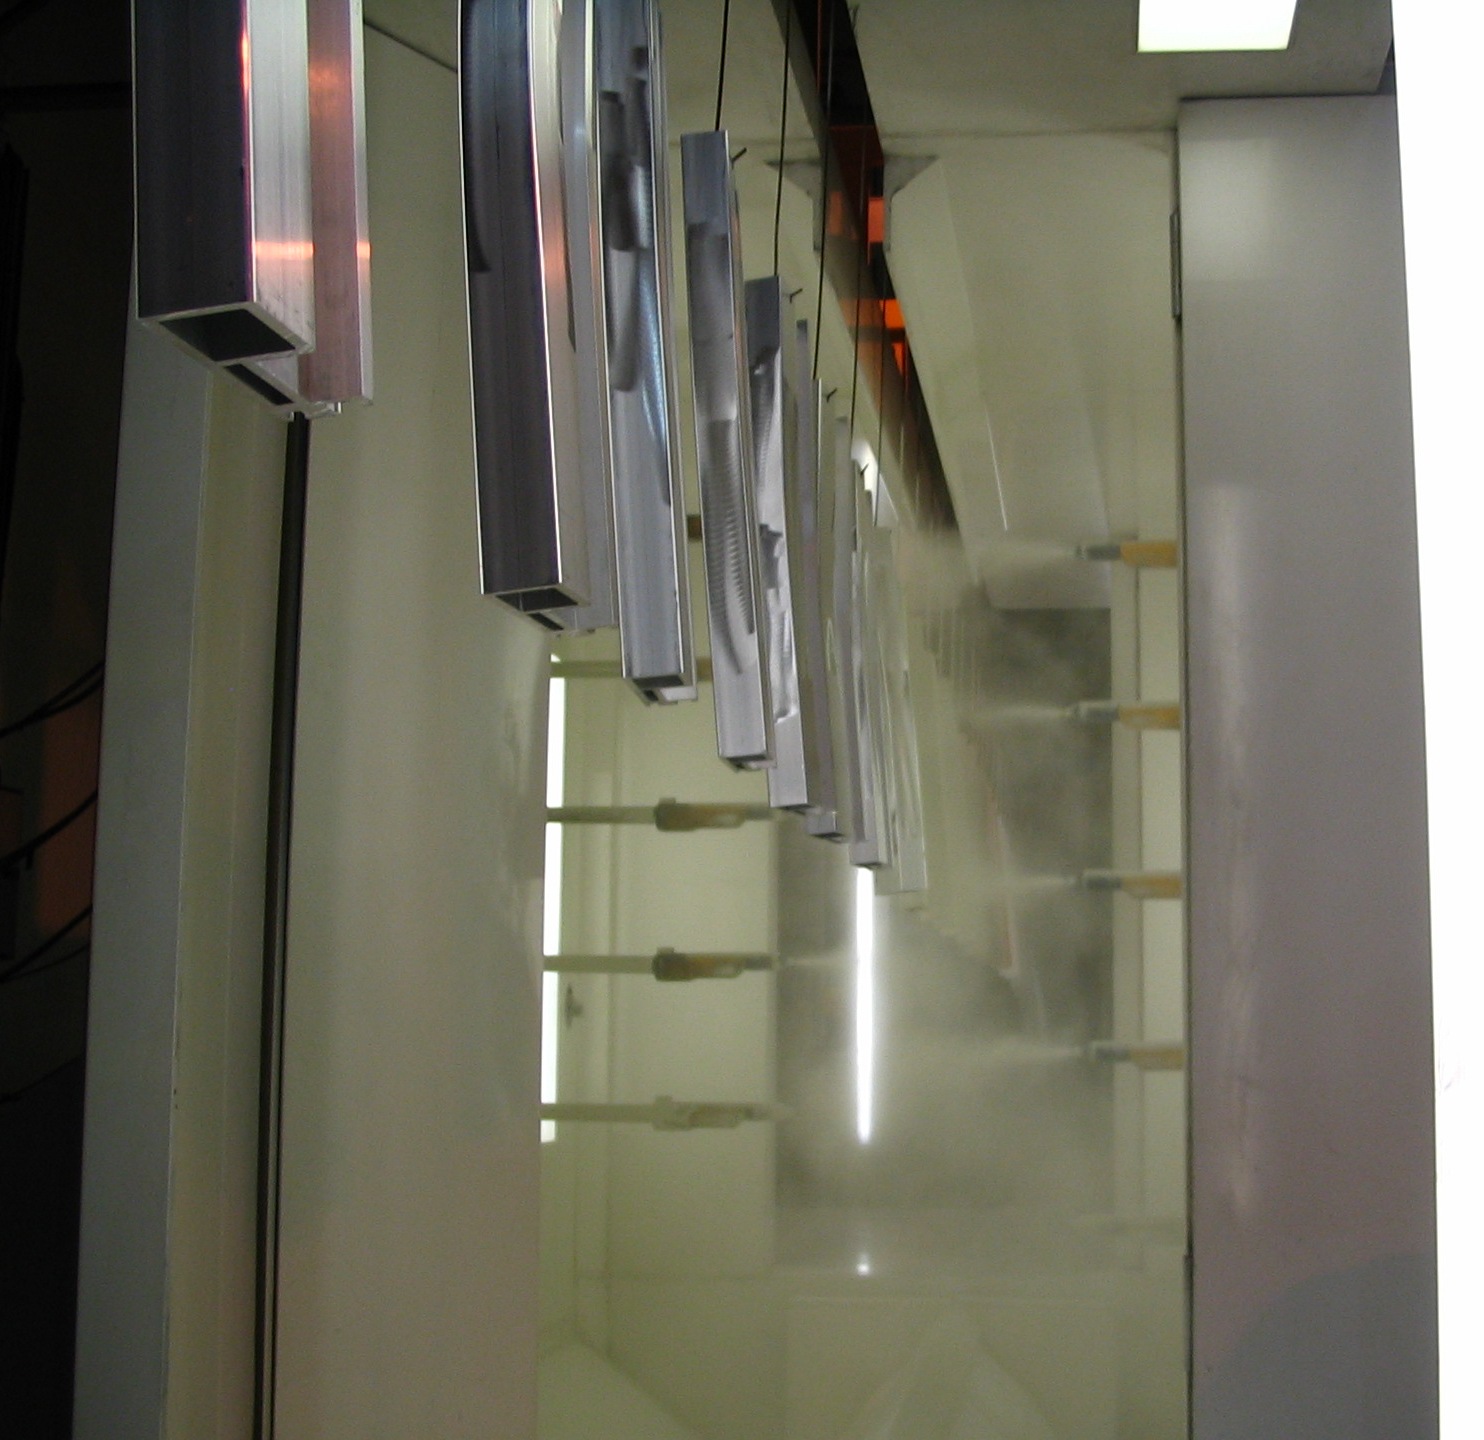
Corrosion Protection
A chromium-free passivation seal closes the phosphate crystal structure immediately after conversion coating, preventing white rust during inter-operation storage and maximising paint adhesion. The sealant chemistry is specified to the downstream paint system and OEM requirement — not selected from a standard catalogue. Salt spray endurance exceeds 1000 hours on qualified systems.
MacroCoats engineers chemistry for every stage of this sequence — not just the phosphating tank.
Bath chemistry drifts. Our system corrects it before you notice.
pH moves, concentration falls, temperature spikes. In a manually-monitored line, those drifts become defects before any operator notices. MacroCoats IoT edge controllers monitor pH, temperature, and TDS continuously — and trigger auto-dosing corrections the moment a parameter deviates from specification.
The result is bath chemistry that holds specification across every shift, every operator, and every season. Not because your operators are more attentive — because the system doesn't wait for them to act.
Read the IoT monitoring deep-divePhosphating: Foundation of Every Surface.
Highest salt-spray endurance in the range. Engineered for Tier-1 automotive OEM requirements where 500-hour ASTM B117 compliance is mandatory.
- Automotive body panels
- Chassis & suspension
- OEM export components
Full zinc phosphate performance at 45°C bath temperature. Reduces energy consumption 30–40% versus standard lines with no loss in coating weight.
- High-volume lines
- Barrel operations
- Heat-sensitive alloys
Workhorse zinc phosphate for pre-paint and pre-powder coat on mild steel. Consistent 1.8–3.2 g/m² coating weight across varied water hardness.
- General fabrication
- Pre-paint lines
Dense manganese crystal for wear-resistant applications. Break-in retention for gears, pistons, and high-torque fasteners.
- Gears & pistons
- Fastener barrels
- Defence hardware
Manganese formulation with advanced sludge-suppression chemistry. Extends bath life and reduces downtime on continuous production lines.
- High-volume Mn lines
- Rail & defence
Single-stage iron phosphate for light-duty pre-paint applications. Short cycle time and minimal maintenance make it suitable for manual spray operations.
- Light fabrication
- Powder coat prep
- Appliance panels
High-throw iron phosphate for recessed profiles and welded assemblies. Penetrates weld seams and geometry that standard spray lines miss.
- Welded frames
- Tubular assemblies
- Motor housings
Clean Surfaces Begin With Smart Degreasing.
Heavy-duty alkaline degreaser for stamping oils, coolant residues, and metallic fines on steel and CI. Free-rinse formulation.
Low-foam alkaline degreaser formulated for high-pressure spray wash systems. Suppresses foam without compromising degreasing efficiency.
Inhibited hydrochloric acid pickle for oxide and mill-scale removal. Over-etch inhibitor minimises base metal attack on thin-gauge stampings.
Titanium colloidal activator that nucleates phosphate crystal growth to 1–2 µm. Dramatically improves coating weight uniformity on deep-drawn stampings.
Iron-specific activation bath for iron phosphate lines. Removes residual alkalinity from the degreaser stage and conditions the surface for uniform Fe conversion.
Final rinse additive that seals the phosphate crystal and extends salt-spray performance without hexavalent chromium. EU ELV compliant.
Aluminium & Steel: Protection Without Compromise.
Chromate conversion coating for aluminium per MIL spec. Maximum corrosion resistance and paint adhesion for aerospace and defence applications.
Trivalent-chromium-free passivation for aluminium. Equivalent corrosion performance to chrome conversion without hexavalent chromium concerns.
Cost-effective aluminium passivation for light industrial applications. Compatible with acrylic, polyurethane, and epoxy topcoat systems.
High-performance chrome passivation for phosphated steel. Seals the phosphate crystal structure and delivers 500+ hours ASTM B117 endurance.
Organic seal system that replaces hexavalent chrome on phosphated steel. Satisfies RoHS, REACH, and EU ELV directives with no performance compromise on tested systems.
Keep Your Bath in Specification.
Dispersant additive that keeps phosphate sludge in suspension, reducing dragout and extending bath drain intervals.
Grain-refining additive for zinc phosphate. Reduces crystal size to below 4 µm for dense, uniform coatings and improved paint inter-adhesion.
Water-displacing rust preventive for inter-operation storage of phosphated components. Thin film, easily removed before final coating.
Industrial Oils & Process Fluids
Temporary corrosion protection for stored and transported components.
High-performance lubrication for bearings, gears, and sliding surfaces.
Specialty oil for electrical transformer maintenance and insulation.
Water-based and semi-synthetic coolants for machining and grinding.
Neat and soluble cutting oils for turning, milling, drilling, and tapping.
Displaces moisture from metal surfaces to prevent flash rust post-cleaning.
Four Reasons Engineers Specify Us.
Formulation Intelligence
Every batch is co-developed with your process engineer. We analyse your incoming water, steel grade, and downstream paint system before recommending chemistry.
Environmental Compliance
Chrome-free passivation, REACH-registered concentrates, and full RoHS/EU ELV certification built in — not added as an afterthought.
Extended Bath Life
Proprietary sludge suppressants and in-bath buffering technology extend bath life 2–3× versus standard concentrates, reducing drain-and-refill downtime.
Resident Process Chemists
We do not have a helpline. We have on-site process chemists who validate your bath at startup, quarterly, and whenever your steel supplier changes.
Let's optimise your surface treatment process.
Whether you're scaling a phosphating line, addressing inconsistency across plants, or moving to chromium-free systems — our team is ready to engineer chemistry around your process.